
Smart Entry, Stock Awareness & Ordering
How VibeCNC protects bits and cuts cycle times using 3-tier smart entry, 2.5D spatial stock awareness, proportional feed scaling, and pocket-first ordering.
Most CNC machining failures and slow runtimes trace back to three avoidable habits: plunging a flat end mill straight down into solid stock, cutting empty air where a previous tool already cleared material, and retracting needlessly to clearance height between every pass. VibeCNC's Rust Wasm CAM engine solves all three automatically.
3-Tier Smart Tool Entry
Flat end mills, downcut/upcut spirals, and ball-nose bits are designed to cut laterally with their side flutes, not drill straight down. Unless you are running a plunge-native operation (Drilling or V-Carving) or explicitly disable ramping, VibeCNC picks the gentlest available entry for every cut:
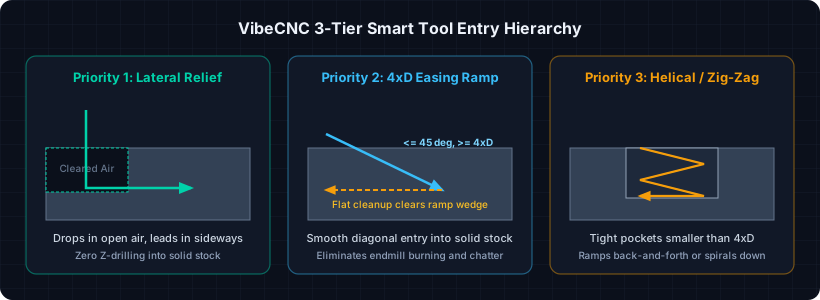
- Priority 1 (Lateral X/Y Relief Entry): Queries the 2.5D spatial stock model for any already-cleared pocket, prior ring, or open air outside the stock boundary at or below the target pass depth. Drops Z cleanly in air, then leads sideways into the material at cutting feedrate.
- Priority 2 (4xD Easing Ramp + Wedge Cleanup): When entering solid stock with room along the path, ramps smoothly over at least
max(4 x bit diameter, pass depth)at an angle never steeper than 45 degrees. Immediately clears the uncut triangular wedge left under the ramp via a forward overlap (closed contours) or flat backtrack (open contours) so the floor is 100% level. - Priority 3 (Constrained-Space Helical or Zig-Zag): Inside narrow pockets or short slots smaller than four bit widths, spirals helically or zig-zags back and forth at a shallow angle down to depth, followed by a flat cleanup lap.
2.5D Spatial Stock Awareness (Zero Air-Cutting)
Before calculating any toolpath, VibeCNC rasterizes all preceding visible toolpaths on the same sheet and side using their actual cutter profiles (flat, ball nose, or V-bit). This unlocks four automatic optimizations:
- Cross-Operation Rest Machining: Toolpath 2 automatically skips air already cleared by Toolpath 1, even across separate independent operations in the Toolpath Tree.
- Dynamic Z2 Rapid Plunge: Instead of feeding slowly from the top of the board down into a deep pocket, the cutter rapids to just above the true remaining material height at the entry XY.
- Safe Stay-Down Linking (
Join2D): Moves directly across already-cleared regions at cutting depth instead of retracting toZ1, while strictly respecting all Keep-Out Clamp zones. - Optional Full-Contact Spring Pass: Stock-awareness is enabled by default. Uncheck Stock-Aware on any individual toolpath when you intentionally want a full-contact spring or finish pass.
Proportional Feed Scaling & Pocket-First Ordering
- Proportional Engagement Feed Scaling: Whenever a bit must take a 100% full-width slotting pass (such as the opening perimeter of a pocket or profile) after being tuned for a 35% to 40% stepover, VibeCNC proportionately scales down the feedrate (
F) on that heavy-load segment so you get clean chips without burning, chatter, or broken 1/8" bits. - Complete-Pocket-First + Nesting-Safe 2-Opt: Finishes every concentric ring and Z-pass of one pocket before moving to the nearest neighbor, while strictly enforcing containment order so interior holes and pockets always cut before the outer perimeter frees the part.